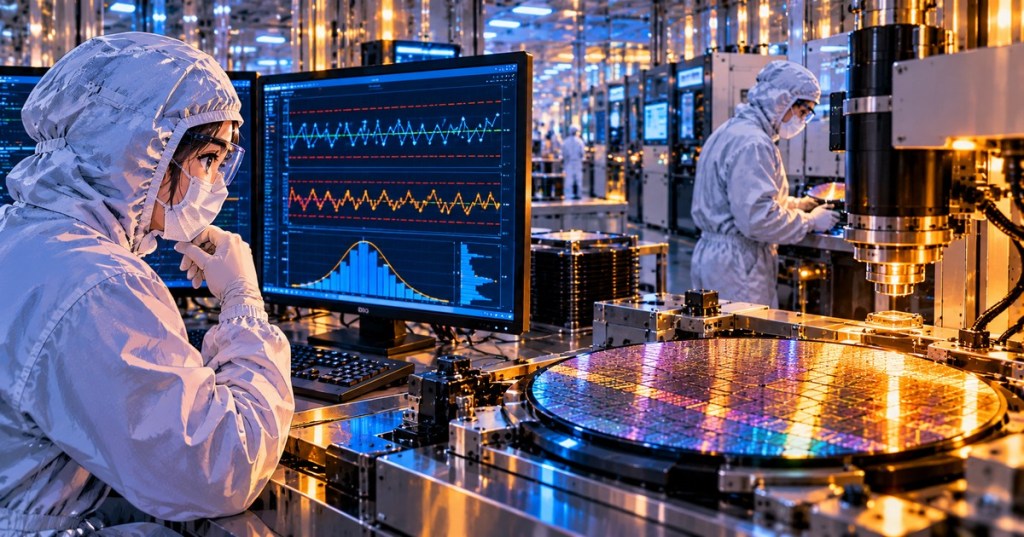
OSSEC.013 — Statistical Process Control in Semiconductor Manufacturing. A semiconductor fab manufactures chips through hundreds of interdependent operations, and a process can gradually drift before a wafer visibly fails inspection. Statistical process control (SPC) is the practice of comparing repeatable measurements with a historical statistical baseline to identify changes that warrant investigation. Unlike an individual wafer’s pass/fail test, SPC examines patterns over time. This chapter follows OSSEC.012 on yield engineering and defect-density models, connects the earlier introduction to control charts with semiconductor metrology, and develops the mathematics of control limits, process capability and engineering response.
Why semiconductor engineers monitor variation
Process measurements can include critical dimension (CD), overlay error, deposited film thickness, sheet resistance, etch depth, particle counts and equipment-state variables. Small movements in these characteristics may have downstream effects, especially where the acceptable process window is narrow. For example, a change in film thickness can alter electrical properties; an overlay shift can move patterned features away from their intended relationship. The quantity to chart must be selected because it has a meaningful link to process behavior or product requirements, not merely because a sensor can produce it.
The NIST/SEMATECH Engineering Statistics Handbook describes SPC as monitoring a current process against its past behavior and deciding when corrective investigation is justified. Recent NIST research also emphasizes in-line metrology and data analytics for semiconductor manufacturing. A fab may combine these methods with fault detection, equipment traces, run-to-run control and wafer electrical test results. The exact data, sampling plan and reaction limits are specific to the manufacturing process and production site.
Common-cause variation and special-cause signals
Common-cause variation is the natural fluctuation of a stable process under its established operating conditions. Special-cause variation suggests a change not adequately explained by the stable historical pattern, such as a changed chamber component, drifted measurement tool, contaminated consumable or altered recipe. A control-chart alarm signals that a process should be investigated; it is not proof of any one of these mechanisms.
In a semiconductor process, identical-looking wafer test results can have different causes. A sudden shift aligned with a maintenance event may suggest one investigation path. A gradual trend spanning multiple chambers may suggest another. Keep timestamps, tools, chambers, recipes, wafer positions, lot identities and instrument revisions aligned before treating a mathematical signal as a physical diagnosis. The American Society for Quality’s SPC training distinguishes common from special causes and warns against unnecessary process adjustment.
Video study — introduction to statistical process control
Operations & Supply Chain Management University presents the foundations of statistical process control: variation, the purpose of charts, and how to think about changes in a process. The video offers general manufacturing context; the semiconductor applications and mathematical safeguards below extend it to fab data.
Control limits are not product specifications
This distinction is central to good engineering decisions. Control limits are statistical boundaries estimated from the process’s own measured history under an appropriate model. The upper and lower limits are commonly abbreviated UCL and LCL. Specification limits, abbreviated USL and LSL, come from engineering, process-integration or product acceptance requirements. The two sets of limits answer different questions: Is the process behaving consistently? versus Is it producing an acceptable result? NIST explicitly distinguishes control limits from specification limits.
A stable process may consistently produce values too close to, or even beyond, an engineering limit. Conversely, all measured values in a short run can lie within the specification while exhibiting a statistically meaningful trend that forecasts a later failure. Do not widen control limits simply to suppress alarms or shrink specification limits to make a stable process appear capable. Document who owns the limits, which baseline is in effect and what process revision they apply to.
The three-sigma framework
In the simplest Shewhart-style setup for a charted statistic w, if the stable historical mean is μw and its standard deviation is σw, the three-sigma limits are UCL = μw + 3σw and LCL = μw − 3σw. The charted statistic might be an individual observation, a subgroup mean or another defined quantity; the correct standard deviation must correspond to that statistic, not be copied from an unrelated dataset. NIST’s variables-control-chart guide explains the basis and estimation issues.
Illustrative chart of a single process statistic, in nm
Stable baseline mean:                   10.00 nm
Standard deviation of chart statistic: 0.10 nm
Upper control limit: 10.00 + 3 × 0.10 = 10.30 nm
Center line:         10.00 nm
Lower control limit: 10.00 − 3 × 0.10 =  9.70 nm

New observed statistic: 10.36 nm
Result: outside upper statistical control limit
These are invented instructional numbers, not actual semiconductor production data. The calculation assumes the 0.10 nm figure is a valid stable baseline standard deviation for the statistic being charted. A recorded 10.36 nm value triggers review of the measurement and process history; it does not, by itself, mean that the wafer is out of engineering specification. Appropriate chart design, subgroup selection, independence, measurement uncertainty and sufficient baseline data matter before applying such rules.
Choosing X̄, R, S and other chart types
When a tool produces repeated measurements in rational subgroups, engineers may chart the subgroup average X̄ to monitor the process center and the subgroup range R or standard deviation S to monitor within-subgroup variability. A rational subgroup groups measurements taken under similar short-term conditions so that its variation can be distinguished from variation between production times, lots or runs. NIST’s X̄/R/S reference provides the statistical factors used to calculate the limits when process variation must be estimated from subgroup data.
A chart of individual measurements may be more appropriate if each run yields one usable reading. A p-chart describes defective fraction under suitable assumptions, while count-based charts can address other data types. Different measurements have different distributional and sampling assumptions. Wafer particle counts, spatially correlated sites, repeated readings of the same object and nonstationary chamber signals may violate the assumptions of an ordinary X̄/R chart. Chart selection is a statistical design decision rather than a software formatting option.
Patterns that merit investigation
A point outside a validated three-sigma limit is a common signal. A long run of readings on one side of the historical center line or a consistent trend can also suggest a shift. Under one family of Western Electric-style rules, for example, eight consecutive points on the same side of the center line can be a warning. These supplementary rules are not universal and affect the false-alarm rate. NIST discusses both their sensitivity and their increased false alarms. Fabs must define the applicable detection rules and response actions before interpreting the chart.
The statistical alert is a trigger for evidence collection, not a command to adjust the recipe. If operators repeatedly correct ordinary random fluctuation, they can increase total variation rather than reduce it. Correlate the signal with verified tool events, measured chamber state, gas-flow controller trends, ALD pulse/purge behavior, contamination observations and the physical limits of the metrology tool.
Process capability — Cp versus Cpk
Once a process is shown to be sufficiently stable for the intended model, process capability compares its spread and position with engineering requirements. For a two-sided approximately normal characteristic, the classical indices use the process mean μ, an appropriate within-process standard deviation estimate σ, and the upper and lower specifications:
Cp  = (USL − LSL) / (6σ)
Cpk = min[(USL − μ)/(3σ), (μ − LSL)/(3σ)]
Cp considers specification width relative to process spread, without accounting for where the mean sits between limits. Cpk includes the shift of the process center toward the nearest specification boundary. The complete treatment in NIST’s capability chapter also distinguishes one-sided specifications and uncertainty in estimated capability indices.
Worked semiconductor example — a critical dimension
Imagine a fictional semiconductor patterning process where a feature dimension must fall between 9.6 nm and 10.4 nm. A sufficiently characterized stable process has mean 10.1 nm and an appropriate standard deviation of 0.10 nm. The specification width is 0.8 nm and the modeled six-sigma process width is 0.6 nm. The capability values are:
LSL = 9.6 nm    USL = 10.4 nm
μ   = 10.1 nm   σ   = 0.10 nm

Cp = (10.4 − 9.6)/(6 × 0.10)
   = 0.8/0.6 = 1.33

Upper-side capability = (10.4 − 10.1)/(3 × 0.10)
                      = 0.3/0.3 = 1.00

Lower-side capability = (10.1 − 9.6)/(3 × 0.10)
                      = 0.5/0.3 = 1.67

Cpk = min(1.00, 1.67) = 1.00
Here, Cp ≈ 1.33 indicates that the modeled spread is narrower than the entire tolerance band, while Cpk = 1.00 shows that the mean lies closer to the upper specification. Centering the process could improve Cpk even without reducing spread. Whether either value is acceptable depends on the approved device/process requirements and evidence supporting the assumptions; there is no single industry-wide cutoff for every semiconductor feature.
A real semiconductor capability study must check sample size, stability, measurement-system uncertainty, distribution shape, within-wafer correlation, lot effects and tool-to-tool differences. NIST notes that capability estimation with small samples can be unreliable and that normal-distribution assumptions matter. Measurements from dozens of highly correlated wafer sites cannot automatically be treated as dozens of independent process observations.
Video study — interpreting Cp, Cpk, Pp and Ppk
CQE Academy’s training video demonstrates why a process’s spread and its centering are separate questions. It also compares short-term capability indices with indices based on overall process performance. The worked CD example above is independent of the video’s data and is provided to connect the general formulas with semiconductor metrology.
Semiconductor metrology changes the interpretation
A wafer fab does not operate like a perfectly independent stream of identical manufactured parts. Measurements are organized by fab, process module, tool, chamber, recipe, lot, wafer and position on the wafer. A drift at the center of every wafer is different from one edge-localized pattern or a shift present only on one chamber. The yield and wafer-map chapter explains why spatial defect patterns carry information beyond a single yield percentage. Metrology and inspection are similarly distinct: metrology quantifies dimensions while inspection searches for defects and contamination.
NIST’s CHIPS metrology program emphasizes reliable, fit-for-purpose measurements, particularly as devices become multilayered and complex. Measurement uncertainty can blur a seemingly small process change. A NIST study on measurement uncertainty and process control explains that metrology errors can cause both unnecessary rejection and mistaken acceptance. Equipment and process engineers should know the calibration status, repeatability, sampling locations and uncertainty budget before confidently interpreting an apparent control limit breach.
From SPC to run-to-run control and virtual metrology
SPC primarily detects statistically significant patterns in observations; a run-to-run control system may use prior measured outcomes to recommend or implement a controlled recipe adjustment for a later run. Fault detection and classification can flag abnormal equipment traces and help localize faults. Virtual metrology estimates a product property using process and equipment sensor information when direct metrology is delayed or sparse. These approaches can work together but are not identical.
NIST researchers have reported online virtual-metrology and dynamic-sampling approaches designed to address drift, changes in sensor behavior and sparse measurements in semiconductor production. Such models still require measurement validation and uncertainty management. A 2026 review of modern semiconductor statistics discusses the use of multivariate monitoring, drift detection, run-to-run control and semiconductor-specific hierarchical data structures. A control chart is therefore one component of a wider process-monitoring system.
Engineering response and evidence handling
- Define the characteristic: record the unit, intended specification, chart type, subgrouping plan, sample location and ownership of statistical-control limits.
- Validate the signal: confirm data integrity, calibration, the correct recipe and baseline, and whether the measurement is reproducible within expected uncertainty.
- Correlate physical events: compare the signal with equipment maintenance, chemistry, chamber state, lot history and environmental conditions.
- Assess risk: determine whether affected material needs review under the fab’s prescribed disposition, hold or escalation procedure.
- Document the outcome: distinguish measured facts from hypotheses and document corrective action and the post-change evidence.
A chart alarm must never become a reason to bypass safety interlocks, modify a production recipe without authorization or conceal suspected quality escapes. The appropriate response depends on site process ownership, change controls and material disposition rules. In advanced device structures such as FinFETs and gate-all-around nanosheets, interacting dimensions make the physical interpretation especially important; one statistical metric cannot summarize the entire transistor.
Knowledge check
- What do UCL and LCL describe, and why are they not interchangeable with USL and LSL?
- Why might a statistically stable process still produce devices outside specification?
- For a process with Cp = 1.33 and Cpk = 1.00, what likely explains the difference?
- Why should wafer position, tool/chamber identity and metrology uncertainty accompany a control-chart alert?
- How does an SPC alarm differ from an authorized run-to-run recipe adjustment?
Answer key: Control limits describe expected statistical behavior under an established process model; specification limits represent engineering acceptance requirements. A stable distribution may be off-center or too wide for the specification. A lower Cpk than Cp indicates that the process mean is closer to one boundary. Wafer and tool context and measurement uncertainty determine whether a signal reflects a localized physical shift or a measurement artifact. SPC detects changes; recipe modification is a separate controlled action.
Primary references and related lessons
The principal references are NIST/SEMATECH: Process or Product Monitoring and Control, NIST: Variables Control Charts, NIST: Shewhart X̄/R/S Charts, NIST: Process Capability, NIST: CHIPS Metrology Program and NIST: Virtual Metrology and Dynamic Sampling. Explore the wider internal knowledge network through Control Charts Help Manufacturers Find Problems Earlier, Semiconductor Yield Engineering, Semiconductor Metrology and Inspection, Deposition Equipment Basics and Mass Flow Controller Diagnostics.
BitcoinVersus.Tech Editor’s Note: We volunteer daily to ensure the credibility of the information on this platform is Verifiably True. If you would like to support our work and help further secure the integrity of our research initiatives, please scan the QR code below to donate 5,000 sats.



Leave a Reply