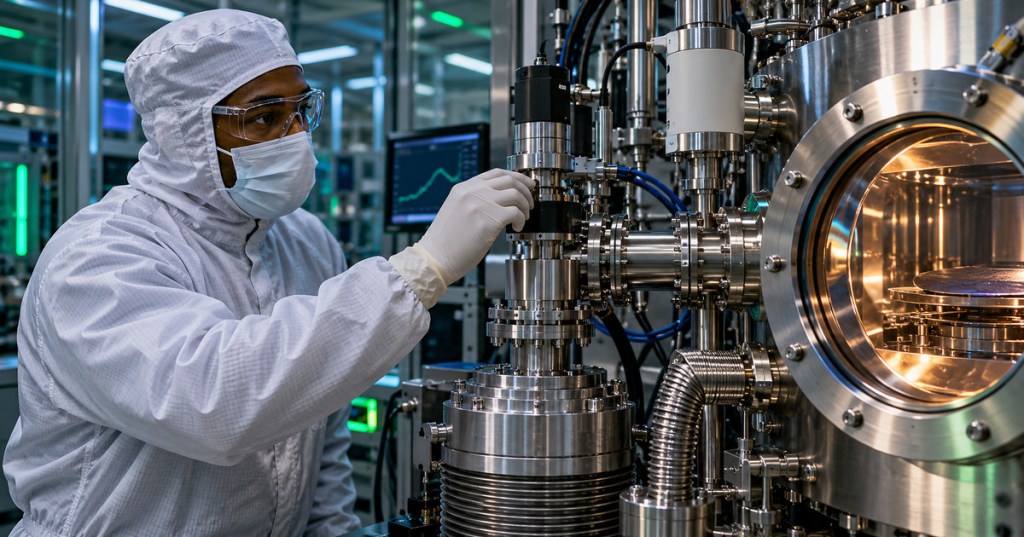
Semiconductor chamber pressure control is the process of holding the gas pressure inside a wafer-processing vessel at a specified level while gases enter and vacuum pumps remove them. Pressure changes can affect gas density, residence time, plasma behavior, film deposition and etching. Technicians therefore examine the pressure sensor, commanded setpoint, throttle-valve response, gas-flow readings and pump condition as one feedback system rather than treating each display as an independent verdict. This lesson builds on semiconductor vacuum systems and mass-flow-controller diagnostics.
Elementary Overview
A semiconductor process chamber is a sealed space where a silicon wafer is exposed to carefully controlled gases. A pump removes gas, but a machine sometimes needs to keep a small, steady amount of gas inside the chamber. A pressure gauge tells the controller how much gas pressure exists; a throttle valve changes how easily gas can escape toward the pump. Together, these devices act like an automatic adjustment system that continually checks whether the chamber is at its target pressure.
A pressure alarm does not necessarily mean the pump has failed. The gauge can be misconfigured, the gas supply can change, the valve may not move correctly, or material in the chamber can release additional gas. The safest first step is to compare recorded measurements and alarm history, not to open the equipment.
Pressure, Flow and the Control Loop
A typical downstream pressure loop contains a process chamber, one or more gas-delivery MFCs, a pressure transducer, a controller, a motorized throttle valve and a vacuum pump. The equipment host transmits a pressure setpoint; the controller compares it with the pressure measurement and commands a valve position. Opening the exhaust valve generally increases conductance toward the pump and lowers chamber pressure, while restricting the exhaust generally raises it when gas continues to enter. The relationship is nonlinear and depends on piping, gas load and operating regime. VAT’s Series 620 manual describes this feedback principle and distinguishes downstream valve control from upstream gas-flow control.
The controller may implement proportional–integral–derivative (PID) or adaptive tuning. A technician should not equate a rising valve-position percentage with a fixed mechanical opening unless the instrument documentation establishes that convention: different actuator interfaces may report position, closure, or percentage travel differently. A valve command is also not proof of physical movement. Correlate target pressure, measured pressure, commanded position, actual position feedback (if available) and event timestamps.
Capacitance Manometers and Pressure Units
A capacitance manometer measures pressure using diaphragm deflection sensed as a capacitance change. It is particularly useful for process pressure because the basic measuring principle is not dependent on gas thermal conductivity. Nevertheless, range selection, zero condition, temperature, contamination, mounting and electronics can all affect the result. Confirm whether a display is showing absolute pressure or gauge pressure and check the transducer’s full-scale rating before comparing process trends.
Common units include Torr, millitorr (mTorr), pascal (Pa), and millibar (mbar). The conversions 1 Torr ≈ 133.322 Pa and 1 mTorr = 0.001 Torr are useful, but pressure-control alarms should be assessed against the recipe’s actual specified units and tolerances. A sensor with the wrong scaling or range may appear to malfunction even when its electrical output is normal.
Manufacturer demonstration: the diaphragm movement inside a capacitive gauge explains why pressure can be measured as an electrical signal and why correct installation and zero checks matter.
Other Gauges and Range Selection
A roughing or pumpdown system may also use a piezoresistive sensor, Pirani gauge, cold-cathode gauge or hot-cathode gauge. These technologies do not necessarily agree over every pressure range. Pirani gauges infer pressure from heat transfer and are gas dependent; capacitance and piezoresistive diaphragm gauges respond to mechanical pressure. Ionization gauges are intended for lower-pressure regimes and need appropriate protection and operating procedures. Pfeiffer Vacuum’s vacuum measurement reference explains these differences.
A gauge cross-check is valuable only if both instruments are specified for the observed pressure and configured correctly. During pumpdown, a gauge may approach the edge of its usable range, causing an apparent flattening or abrupt transition. The second manufacturer video illustrates how pressure changes resistance in a piezoresistive sensing diaphragm; it is an instructive comparison with the capacitance principle above.
Throttle Valves, Conductance and Pumping Speed
A throttle valve does not create vacuum. It changes the flow conductance between the chamber and the pumping system, thereby changing the effective pumping speed at the chamber. A restriction can make a healthy downstream pump appear ineffective at the chamber connection. Conversely, a valve stuck open may prevent the controller from maintaining a higher process-pressure setpoint if gas input is limited. The MKS Type 653B manual documents an exhaust throttle valve working with a controller and capacitance manometer in a closed loop.
For a simplified steady-state chamber, gas throughput and effective pumping speed satisfy Q ≈ p × Seff, where Q is throughput in Torr·L/s, p is pressure in Torr and Seff is effective pumping speed in L/s. For an illustrative gas throughput of 1.0 Torr·L/s at 0.5 Torr, the effective speed is approximately 2.0 L/s. This is a model, not a field-calibration method: real chambers include pressure-dependent conductance, gas species, outgassing and changing flow conditions.
Understanding Pumpdown Traces
Pumpdown is the reduction of chamber pressure after a permitted evacuation sequence. In an ideal well-mixed volume V with constant effective pumping speed S and negligible gas input, pressure decreases approximately as p(t) = p(0) × exp(−St/V). Its characteristic time constant is τ = V/S. For an illustrative 100-liter vessel with effective pumping speed of 20 L/s, τ is five seconds; after 15 seconds the ideal model predicts about five percent of the starting pressure. Actual process chambers can depart substantially from this model as flow regimes change, valves move, seals leak and surfaces release adsorbed gas.
When a pumpdown curve stalls above the expected value, examine the foreline and chamber pressure together, then compare pump state, valve status, gauge range, isolation status and scheduled vent/purge events. A slow curve alone cannot distinguish a leak from outgassing, restricted conductance, an incorrect sensor range or inadequate pumping. Chamber deposits and contamination can complicate repeatability, and ALD pulse-and-purge traces should be interpreted in the context of the recipe step.
Practical Read-Only Diagnostic Workflow
- Confirm the equipment ID, recipe step, permitted operating state, active alarms, pressure setpoint and the unit of measure.
- Compare pressure feedback with an appropriately ranged independent gauge where the equipment provides one. Record whether both channels use compatible absolute-pressure scales.
- Review MFC setpoint and measured flow, pump/foreline status, valve command and actuator feedback over the same timestamps.
- Note whether the fault appears during steady pressure hold, gas introduction, valve movement, venting or pumpdown; do not compare traces from unlike recipe steps.
- Check documented controller status and sensor/actuator fault flags. Escalate suspected calibration, physical restriction, leak or actuator defects under the site’s authorized maintenance process.
A symptom of persistent high pressure with the throttle valve driven toward its most open verified state can indicate insufficient effective pumping, excess incoming gas, a leak, outgassing or a measurement problem. Oscillation around setpoint suggests examining feedback delay, valve motion, changing gas load and tuning, but does not justify changing protected parameters without approval. A sudden discontinuity in only one gauge suggests checking sensor health and range before altering the mechanical system.
Safety, Interlocks and Contamination
A semiconductor vacuum chamber may contain toxic, corrosive, pyrophoric or oxygen-displacing residues even after processing stops. Vacuum assemblies may also store electrical, thermal, mechanical and pneumatic energy. Do not open gas lines, defeat interlocks, bypass exhaust protection, loosen process-exposed flanges or force a control valve while interpreting an alarm. Follow the site’s qualified-service authorization, equipment procedures, contamination control and OSHA hazardous-energy-control guidance. This lesson addresses trend interpretation, not invasive maintenance.
Knowledge Check
- What is the difference between pressure setpoint and a pressure-transducer reading?
- Why can a fully open throttle valve fail to produce the expected chamber pressure?
- What do Q, p and Seff represent in the simplified throughput relation?
- Why might a Pirani gauge and capacitance manometer disagree?
- What trends should be preserved before a technician escalates a chamber-pressure alarm?
Answers: The setpoint is the requested target; the transducer reading is measured feedback. A valve cannot compensate for inadequate pump speed, excessive gas load, restricted plumbing, outgassing or inaccurate measurement. Q is throughput, p is chamber pressure and Seff is effective pumping speed. Different gauge technologies have different operating ranges, gas dependencies and calibration characteristics. Preserve time-aligned setpoint, pressure, gas-flow, valve, pump and alarm traces.
Elementary Conclusion
Chamber pressure control keeps the amount of gas inside a wafer-processing machine close to the amount a recipe requires. A gauge measures pressure, a controller compares the measurement with a target and a throttle valve helps regulate how quickly gas leaves for the vacuum pump. When pressure changes unexpectedly, the problem can come from any part of that chain.
The important technician skill is to read several signals together before drawing a conclusion. Comparing the gauges, valve response, incoming gas flow and pumpdown history helps identify what changed without putting people or equipment at risk.
Primary References and Related Lessons
Technical references: VAT Series 620 installation and operating manual; MKS Type 653B exhaust throttle valve manual; MKS Baratron selection and installation note; and Pfeiffer Vacuum measurement fundamentals. Continue with plasma etch equipment, deposition equipment, and MFC diagnostics.
BitcoinVersus.Tech Editor’s Note: We volunteer daily to ensure the credibility of the information on this platform is Verifiably True. If you would like to support our work and help further secure the integrity of our research initiatives, please scan the QR code below to donate 5,000 sats.

For the best scanning results, open this page on a laptop or larger screen and use your mobile Bitcoin wallet to scan the QR code. Verify the recipient address before sending.
BitcoinVersus.tech is not a financial advisor. This media platform reports on financial subjects purely for informational purposes.


Leave a Reply